We manufacture precision hydraulic cylinder pistons for heavy equipment and industrial machinery, and custom hydraulic systems.
From drawings, samples, or worn components, DREJEX provides reliable replacement pistons with accurate dimensions andapplication-focused machining.
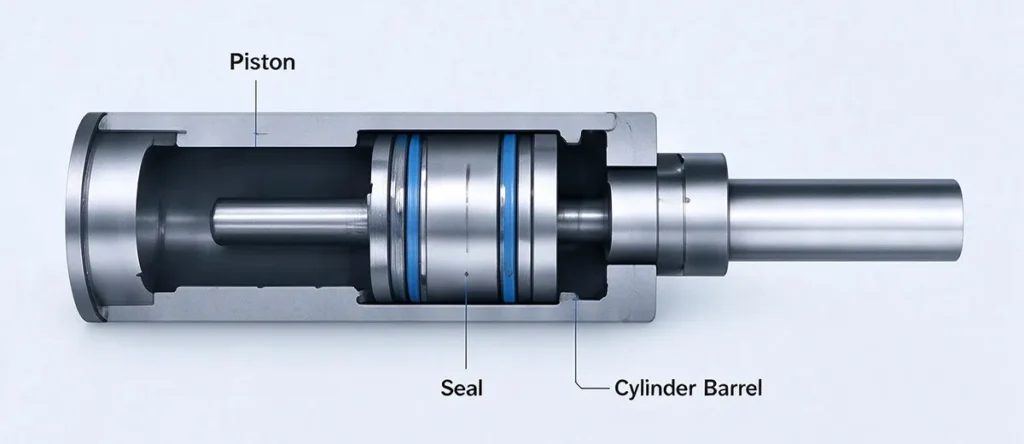
Hydraulic cylinder pistons are precision-machined components that transfer hydraulic pressure into linear motion inside a cylinder assembly.The piston works together with piston seals and the cylinder bore to maintain pressure, reduce leakage and ensure smooth operation.
For aftermakert replacement projects, pistons are often required when original components are worn, damaged, discontinued or unavailable.
We don’t just sell standard parts. Whether you have a complete technical drawing, a worn sample, or just basic dimensions, our engineering team can produce the exact piston you need. We support both standard and non-standard specifications for heavy-duty applications.
From light-duty replacements to heavy-duty custom machining, we deliver the exact piston your system requires.
Standard light-duty piston with narrow profile. Features precise O-ring grooves for smaller hydraulic cylinders and low-pressure applications.
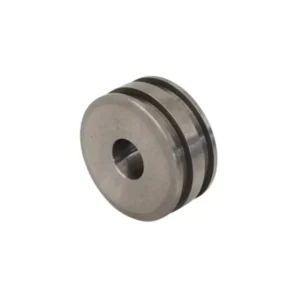
Heavy-duty wide profile engineered for high-pressure systems. Deep grooves accommodate U-cups and wear rings for extreme loads.
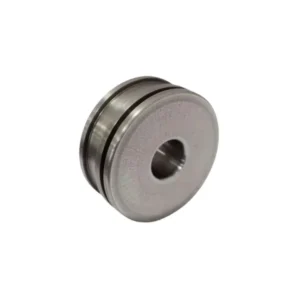
Standard single wear ring design. Optimized for precise fitting and smooth reciprocating motion in standard industrial cylinders.
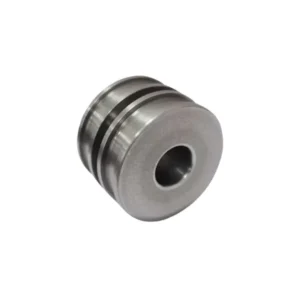
Premium double wear ring configuration. Provides superior stability and load distribution for heavy equipment aftermarket.
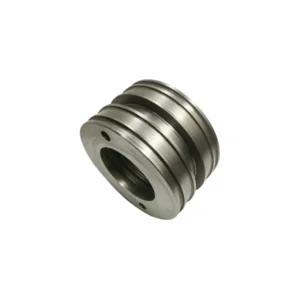
Our most popular wholesale option. Machined from EN-GJS-500-7 ductile iron to withstand extreme wear. Ideal for aftermarket replacement.
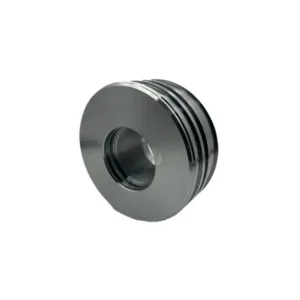
No drawings? No problem. We specialize in complex threaded or non-standard parts. We reverse-engineer from your worn sample.
Our custom ductile iron and steel pistons are widely used in high-pressure hydraulic systems across severe working environments. They are critical for maintaining the power and reliability of heavy machinery.
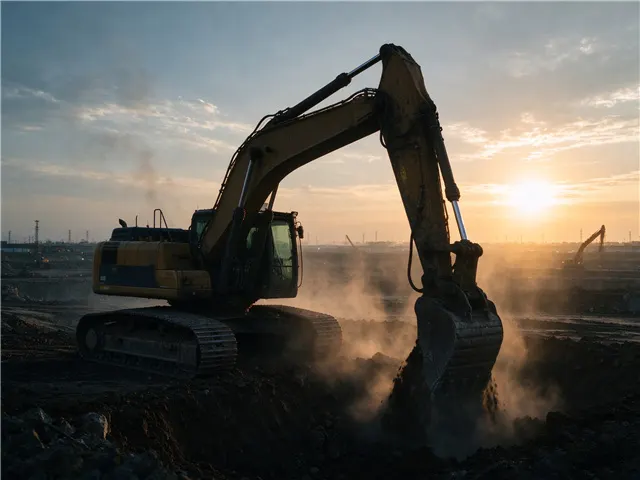
Boom, arm, and bucket cylinder applications.
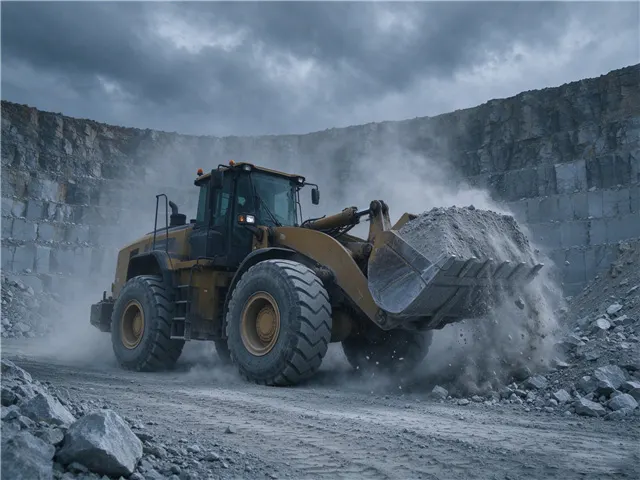
Steering and articulation cylinders.
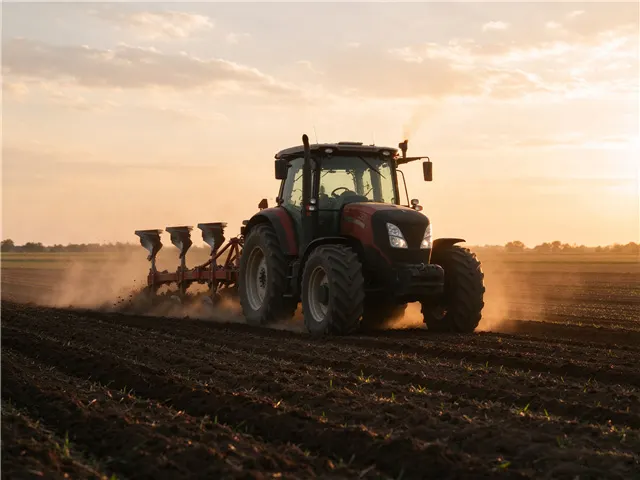
Tillage and implement connections.
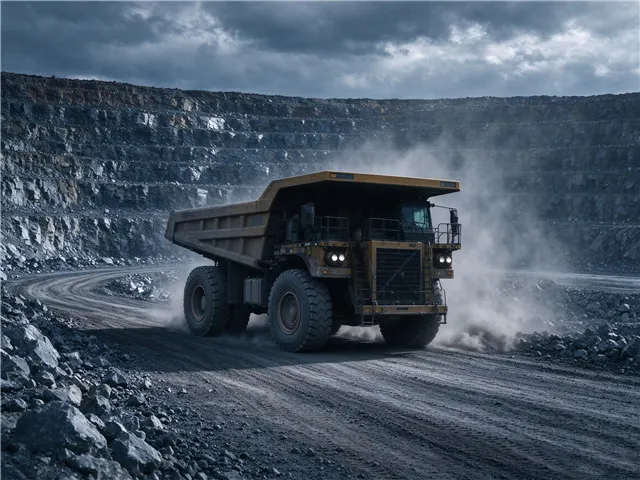
High-load and high-wear applications
We offer a range of materials to meet your specific performance, wear, and environmental requirements.
Excellent wear resistance and high tensile strength.
High strength and durability for general hydraulic applications.
Superior hardness and load capacity for extreme high-pressure environments.
Corrosion resistance for harsh or outdoor environments.
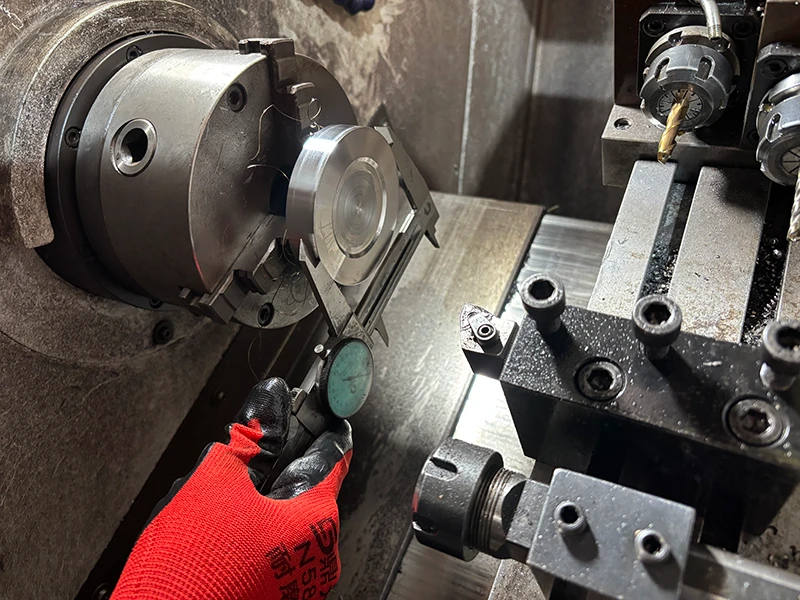
With advanced CNC equipment and experienced technicians, we control key details such as diameter, groove position, and surface finish to ensure consistent quality and reliable performance.
Precision turning controls piston diameter and overall geometry.
Accurate seal grooves ensure proper seal installation and performance
Contolled surface finish supports smooth movement and reduced wear
We don’t replace your existing suppliers. We solve the jobs they can’t.
Our machined pistons act as moving pressure boundaries. This piston body isolates rod-end and cap-end pressure chambers. Pressurized fluid pushes the piston face, generating linear mechanical force. Typical applications involve continuous operating pressures of 21–35 MPa. Precise f7 outer diameter tolerances prevent fluid bypass. High-tensile material properties prevent groove wall deformation under pressure. Strict dimensional stability stops seal extrusion during alternating stroke cycles.
We machine solid raw alloys for specific structural loads. Our material properties table outlines core mechanical strengths.
| Material Grade | Heat Treatment Standard | Tensile Strength (MPa) | Yield Strength (MPa) | Core Application |
| C45 / 1045 | Normalized / Quenched & Tempered | 570 – 700 | ≥ 340 | Standard industrial cylinders |
| 40Cr / 5140 | Quenched & Tempered (Q&T) | ≥ 980 | ≥ 785 | Medium-duty fluid power systems |
| 42CrMo / 4140 | Quenched & Tempered (Q&T) | ≥ 1080 | ≥ 930 | High-impact hydraulic systems |
| SS304 / SS316 | Strain Hardened / Annealed | ≥ 515 | ≥ 205 | Corrosive marine environments |
DREJEX turns diverse structural piston variations into your customized prints. Review our design profiles and precision focus below.
| Piston Structure | Design & Functional Profile | Precision Machining Focus |
| Double-Acting Pistons |
• Bilateral pressure shoulders • Dual-directional seal grooves • Integrated wear ring tracks |
• High-precision dual-groove concentricity • Precise shoulder turning avoids side-loading |
| Single-Acting Pistons |
• Single pressure face configurations • Integrated return spring pockets • Gravity-return shoulder guides |
• Optimized unidirectional loading geometries • Strict spring seat alignment prevents binding |
| Telescopic / Multi-Stage |
• Concentric multi-stage sleeves • Dynamic nested pressure seals |
• Strict sleeve wall-thickness tolerances • Exact sizing guarantees smooth sequential staging |
| Plunger & Ram Assemblies |
• Heavy-duty solid steel structures • Direct shaft-to-bore sliding contact |
• Controlled induction case hardening • Long-stroke grinding ensures consistent outer sizes |
| Tandem / Booster Pistons |
• Multi-piston assemblies • Single continuous rod mounting |
• Perfect axial bore center alignment • Precise inline turning prevents mechanical binding |
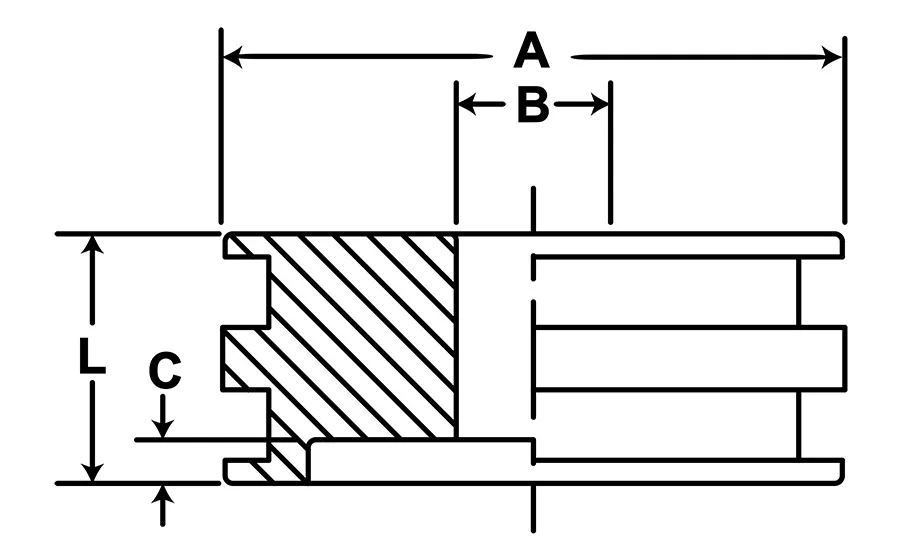
DREJEX details core grooving processes and connection threads.
Cylindrical grinding keeps piston roundness within 5 μm ovality limits. This clearance fit matches your cylinder tube inner wall. DREJEX stops internal fluid bypass during continuous high-pressure cycles.
We finish groove side walls to Ra 0.4–0.8 μm roughness. This turning method removes microscopic machining burrs. Smooth groove flanks reduce dynamic seal wear.
We hold groove depth and width tolerances within ±0.05 mm. Tight tolerances stop seal extrusion during heavy stroke operations. (Note: DREJEX machines steel piston bodies without supplying dynamic seals.)
Piston connection zones must endure continuous compressive stress. DREJEX machines multiple dynamic mating profiles with strict concentricity.
Our lathes mill concentric internal threads against bending stress. Precision-bored pin holes hold zero-play mechanical locking. Ground step shoulders distribute dynamic axial thrust loads evenly.
DREJEX solves critical piston failures and bypass leaks through precise custom machining.
| Failure Mode | Root Cause / Quality Risk | DREJEX Machining Countermeasure |
| Cylinder Scuffing & Bore Galling | • Angular misalignment creates lateral load. |
• We hold piston outer diameter runout below 0.02 mm. • Machinists align thread perpendicularity. • Coaxial assembly stops lateral piston wear. |
| Fluid Bypass (Internal Leakage) | • Clearance deviations cause internal leaks. |
• CNC grinders hold roundness within 5 μm ovality limits. • Rigid machining holds tight metal clearances. |
| Thread Shear & Connection Failure | • Thread stripping occurs under pressure peaks. |
• We mill connection threads. • Tapping creates stress concentration. • Heat-treated 42CrMo alloy steel increases shear strength. • Precise thread pitches stop connection loosening. |
| Wear Ring Groove Flank Wear | • High side loads deform soft groove flanks. |
• We turn tough 42CrMo alloy steel. • Polished groove flanks reduce dynamic wear. |
| Piston Face Cavitation Erosion | • High-velocity fluid changes erode metal faces. |
• We machine smooth radius transitions. • Hardened piston faces withstand cavitation. |
| Snap Ring Groove Shear | • Sharp groove corners concentrate stress under high axial loads. |
• We machine precise radius corners in snap ring grooves. • This geometry distributes axial stress. |
| Piston Body Fatigue Cracking | • Internal defects cause structural failure during high frequency cycles. |
• DREJEX selects ultrasonic-tested raw steel. • Proper quenching and tempering stops crack propagation. |
| Sliding Surface Abrasive Wear | • Contaminated hydraulic fluid scratches soft metal piston lands. |
• We apply HV850 hard chrome plating. • Cylindrical grinding creates a wear-resistant sliding barrier. |
Get answers to common questions about our custom hydraulic cylinder pistons. From material selection like ductile iron and carbon steel to precision tolerances and MOQ requirements, learn how DREJEX meets your specific engineering needs. If you need further technical support, we are ready to help
Why Source From DREJEX?
✓ Custom machining based on your drawings or samples
✓ High-tensile ductile iron and alloy steel options
✓ Strict tolerances (f7/f8) for perfect seal fitment
✓ Flexible MOQ for both wholesale and OEM replacement
✓ Fast turnaround and engineering support
A: Yes. As a direct custom factory, we supply both small batches and wholesale quantities of ductile iron pistons for distributors and repair facilities globally.
A: Absolutely. We can reverse-engineer a new replacement piston based on your worn sample or even basic dimensions. We’ll handle the measurement and drawing for you.
A: We are small-batch friendly. For custom replacement parts, we can accommodate low MOQs to support your specific repair or testing needs.
A: We primarily machine Ductile Iron (EN-GJS-500-7), Carbon Steel (1045), 4140/40Cr, and Stainless Steel.
A: Yes, we can manufacture pistons that perfectly match your original OEM specifications in form, fit, and function.
A: We machine seal groove depths to exact print limits. Digital micrometers check groove walls during active turning. This precise sizing stops oil from escaping behind your dynamic seals. Our shop runs 100% size and roughness gauge inspections before packing.
A: We buy EN-GJS-500-7 raw iron castings from verified local foundries. DREJEX runs ultrasonic tests on every block before lathe work. This testing catches internal air bubbles early. You avoid invisible metal holes leaking under heavy stress.
A: In our experience, misalignment causes uneven piston wear. DREJEX uses rigid centerless grinding machines for finishing steps. We keep outer diameter concentricity strictly below 0.02mm. This alignment guides your piston head straight along the inner cylinder tube.
A: We grind the dynamic sliding faces to an Ra 0.2-0.4 μm finish. This smooth surface prevents premature wear on the hydraulic piston seal side. Our lathes maintain stable cutting speeds without leaving tool vibration marks. Your seals last longer during fast cycles.
Send us your drawings, samples, or requirements. We’ll review your application and provide a practical, cost-effective manufacturing solution.